The creative inspiration for Day 7 came out of necessity today, I had yet another Key given to me, and it was starting to get to the point of madness with all my key-rings and fobs. I decided to make it easy to recognise my keys at a glance and hopefully be able to remove some of my key-ring-trinkets.
I'm calling them Key Skins, and before you say, I know you can buy things a bit like this, but I wanted to make them *custom* and different coloured, also I wanted them to fit my keys and not take up too much extra space.
The first job was to simply scan my keys, import the image into Sketchup and trace around the outline of the key, much easier then measuring anything.
Then just extrude the outline and put a top on it. I made the internal dimension 2.6mm as most keys seem to be under 2.5mm thick.
Within 15 minutes I had the basic Key-Skin for the two most common shaped keys I have.
Quick Print, and they fit well.
Add some extra identification (H = House, G = Garage etc.)
The possibilities are endless! I'm sure you can think of more uses for Key Skins - Files are up on Thingiverse
Print them in Bright fluorescent colours if you always loose your keys!
For Day 6 of 30 days of creativity ( #30DoC ) I'm having a rest from designing things, but I wanted to give my printer a challenging print while I worked.
A few weeks ago I did a quick test print of the Ball of StarsCreated by @Dizingof
I used basic support structure and low-grade PLA just to test it out.
I have been meaning to print another one, much bigger and with full support structure. Today I set it off to print while I worked. It would have been a 17+ hour print, but 9 hours into it, at about half way it shifted on the Y axis, probably due to the head catching on the massive structure with the rather high acceleration settings I use on MendelMax.
Some of the support removed.
You can see that about 40% into the build the Y axis shifted, so when I came home I stopped the print.
Before removing support - This is what it looked like after 9 hours of printing (the half a ball of stars is inside there somewhere!)
This was my first test print a few weeks back, I didn't clean all the support structure off, and it had some unsupported areas, this was sliced with Skeinforge V46 using external support structure at >60 degrees overhang giving me some sections that sagged when they printed in free space.
For the new print today, I made it 150mm wide and enabled support everywhere, as you can see from the above Visual Gcode (Repetier Host) it was a real monster! Skeinforge had to slice for almost 2 hours to output the Gcode for it.
In hindsight a little too ambitious and I should have slowed down the travel moves and enabled Z Lift (Hop) I think it would have printed OK if I had done that.
Doing the same model in Slic3r with support enabled only gives a support column in the centre of the model, so I could not use Slic3r for this print unfortunately, a real shame as it slices in just 8 mins.
It is fun watching these things print.
And it used a fair bit of PLA.
Removal of the support structure is quite easy, but takes a little time.
It needs a little more support removed, but I'm quite happy with how it came out, and it would have looked really good as a complete model and not for the Y Axis Shift.
My proposed new settings for a future print attempt -
I have sliced it again and this time enabled Z lift (Hop) and used Exterior Only support with a 45 Degree minimum support angle, this should give me some support on almost everything, but not cover the entire model.
These are my support settings shown above, if anyone can give any advice to improve these, do get in touch or leave a comment, I hardly ever use support, so could do with any pointers you have.
It still looks like a lot of material, but compare the Gcode image below with the failed print above -
Fingers crossed, it should print well next time, and have a lot less support material to remove.
I woke up today and had an idea for a simple way to join lots of tiny sections of plastic printing filament together, so I thought I would give it a try for Day 3 of
30 days of creativity ( #30DoC ).
Ever since my first filament joiner I have been thinking about easier ways to simplify the process. It's quite hard to join sections smaller than about 50mm manually and I always wanted a simple way to change with lots of colours every layer of an object, that would indeed look totally great! Filament joiner here on Thingiverse if you fancy making one.
So my idea was to use PTFE tube (6mm outer and 3mm inner) to hold tiny cut sections of 3mm printing filament and pop the coiled tube in an oven to fuse the sections together, all sounds perfectly dandy and totally awesome? it should work? right?
Cutting sections of PLA and inserting into the tube was no problems at all.
I had a 1.2M coil of PTFE tube and lots of tiny sections of filament.
It coiled easily and fitted in the oven, heated up and the filament started to melt.
It has a little oozing at each end and I could see the sections were not fusing together as I had hoped.
Exactly the opposite was happening, they were moving apart from each other.
The PLA was getting nice and soft, unfortunately so was the PTFE tube. I removed it and tried to push a 2.5mm metal rod up the tube, this didn't work and I concluded the tube was just too long.
I cut the tube in half and popped it back in the oven, this time it worked a little and I had a section of joined filament out the other end. Then the PTFE tube cooled down and trapped my rod inside the tube stuck to the filament!
I had a few more attempts, but each time the sections that came out were not fused well enough together or the PTFE tube swelled and got jammed up.
I'm pretty sure that PTFE tube elongates as it heats up, and as my PLA sections were not constrained in the tube they also moved along the tube or generally decided to not want to fuse together and actually shrink in length while getting a little fatter in diameter.
So could blocking one end of the tube with a M3.5 bolt and then compressing the filament the other end as it heats up give a single filament? well worth a try at some point?
Or maybe the tube needs to be quickly cooled down so the contraction helps form the filament?
Or possibly the filament needs to be squashed down the tube while still hot and then allowed to cool. (I'm thinking that it will never come out again then)...
Or just maybe the hot tube and contents needs to be passed through a number of aligned sets of bearings squashing it and it's contents to allow fusion and also reducing the filament inside a little to give it a fighting chance to get the damn filament out of the tube again!
Thinking about it now as I type this, it's the same problem we get when the thermal insulator of a hot-end is above 60 degrees C, the PLA jambs up and refused to slide so it could just need to be mechanically stretched after fusing inside the tube while it's still all hot, the bearing die idea may actually work...
So it failed... but I still wanted to post the idea as someone out there may well be able to make it work.
It could have been great! If I get more time I'll try again, Ideas anyone?
Don't forget to take a look at all the other wonderful work for 30 days of creation, * be inspired *
#30DoC the story so far - Day 1 - Day 2 -Day 3 -
This is really going to bug me now...I was dreaming of printing a rainbow Giraffe for you all :(
You gotta fail a bit or you're not trying hard enough!
If you are new to 3D printing, take a look at my Blog and on the RepRap Wiki pages.
If you want to explore the sorts of things you can print with a 3D printer, take a look at Thingiverse
Here is how it was designed and printed -
Open up Sketchup and import a picture you wish to trace or use for inspiration (File-import - Jpg)
Go to 'View' menu bar face-style and select X-ray, this will allow you to see the picture below any 3D objects you place over the image, you can trace around things or align parts to the image.
You can now draw circles and add text, push-pull the various sections to make the model.
With this badge it's going to be printed face down so the text and the X are pushed into the face, allowing for the second colour layer to be seen from the front.
We need to draw and add a simple safety pin clip holder on the back - we will insert the clip while printing!
Export 3D model, slice it and print it out, starting with yellow plastic.
After about 7 layers or while it's still doing the last of the text outlines, switch over to Black plastic.
Let it print the rest of the back and get ready to pause printing when it has done some of the clip.
After is has printed half of the clip when it has a channel, pause the printer while it's doing an infill and insert a safety pin into the channel and tape it in place. Resume printing
The pin will be trapped and after it's cooled down you can wear your badge with pride, and it's bound to bring creative inspiration for the rest of the month.
A very simple guide to making models that are manifold (valid) for 3D printing -
While I was making the badge in Sketchup I had some of the usual errors you get when joining sections of modelled parts together (the text onto the badge face), so as a guide and tutorial here are a few notes about how to make a simple 'manifold' object for 3D printing.
Background -
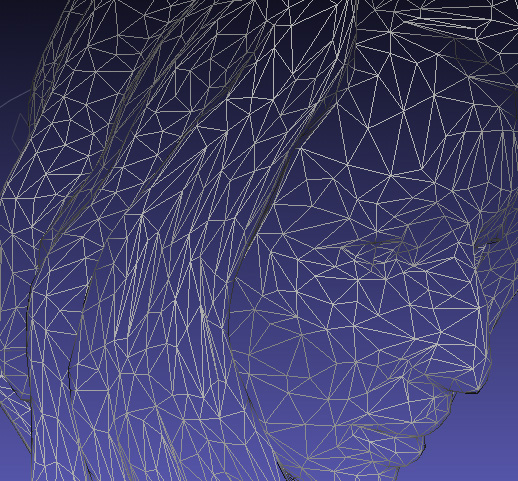
Objects for 3D printing are usually .STL files, the information in a STL file describes the 'mesh' of the model using points and faces, basically made up of lots of triangles joined together describe the surface and contours of the model.
Typical model 'mesh'
Unlike a photo with a set maximum resolution, you can print a 3D model at any size you like, the triangles just get bigger, so you don't gain or loose detail and with most current fused filament 3D printers, if you enlarge a good model you will see more features being printed that were not possible with a smaller size due to the nature of the filament printing process.
This means that the model has a 'Quality' depending on number of triangles describing the surface, I will go further into model quality in another post shortly, but a basic example is shown below -
Top model uses many triangles and can be considered high resolution, middle is half the quality of the top and the bottom is a quarter of the quality / resolution.
Back to valid meshes -
If the mesh is valid and said to be 'manifold' is will have a surface without any defects, these can be holes in the faces, triangles that intersect each other, faces that share the same plane and other odd things like triangles or objects inside other complete meshes that basically make the object invalid.
If a 3D mesh has a problem, it's usually called a 'non-manifold' model, these can be repaired using programs like Netfabb but when designing 3D objects to be printed it's best to try and find and fix problems in the source rather than attempt to repair them later.
Many 3D modelling programs will allow you to join (union) objects together, (the basic free Sketchup does not let you do that automatically) programs like Autocad123D should make a valid mesh out of the two objects, and all you may need to do is remove the part of the object that was not part of the union. But it's always good to be aware of potential issues with 3D.
Example with two cubes - Step 1
We start with two cubes both are components to make it easier to move them together and so they won;t interact unless you want them too.
Step 2
The two cubes have been pushed together, this has made a non-manifold mesh, the cube faces are intersecting each other, so this would not print as you woudl expect from the above image.
Step 3
If you delete the front face you can see the problem.
Step 4
To fix the problem we are going to draw lines around the cube on the surface of where they meet, the red section inside the box is now the problem, but as we have just isolated it, by drawing the lines around the meeting point we can now remove it.
Step 5
After deleting the red cube, you still have a face inside from the dark grey cube, you need to delete that next.
Step 6
Now you have a hollow mesh of the two cubes, this is almost a valid object, you just need to replace the front face by drawing a line down one side and it's done.
here is a progress update on my British Prusa Mendel build - (It's almost finished)
And just to get the chronology correct - This is the 1st son (Daughter?) of 'Mendel Bling' (Bling also has 12 other children in the big wide world) - Bling was the first offspring of 'Bath Mendel' - confused? - good, carry on -
Inspired and encouraged by comments and feedback on my Mendel Bling build and the wonderful colourful Faberdashery plastic that is also manufactured right here in the UK, I have designed and printed a British themed LM8UU Prusa Mendel.
The aim and purpose of this exercise is to promote local design and manufacture of everything and anything.
Wherever you are in the world !
I hope you like how it turned out...
One thing to note is the X carriage size of 450mm wide instead of the normal 406mm, this allows more movement for the Extruder - Allowing a dual extruder set-up to print over the entire build surface.
The X Carriage is of the 4 Linear bearing design - also allowing for future upgrades.
I wanted to try a few new different techniques in this design for getting interesting looking prints, the first was a double sided colour print on both the top and bottom, after some thought, it made sense to print the top as normal, and print out a second section that could be bonded onto the underside.
So this is my plate of frame Vertex parts with the British flag as a layer selective colour section, in the real print I also added some colour stripes to the vertex body (See below).
(It's quite long, so skip bits if you wish, but please take a look at the end results)
Then I needed the other side set of flags to bond onto the vertex, again done in Sketchup and plated up as a single print job.
The Square flags are for another experimental technique, intended to be hot-wrapped around the Z mounts to give horizontal colouring, I need to experiment more with this process.
And spot the obvious mistake, I had a different layer sequences in the Square flags and the Vertex flags when I designed them, so the white and blue colours are accidently reversed on the Square flags, Doh!
The flag is only 2.4mm thick so it was bonded with heat onto the six Vertex pieces.
X carriage motor end with LM8UU linear bearings on the Z Axis.
All other parts are printed in a Blue, White, Red, White, Blue sequence.
Again a short video on the other printed parts - Check it out in Hi-def on Youtube Here of view below -
I also wanted an identification plate and some status indicators for the machine.
Designed in Sketchup, it's going to cover almost all my build area.
This was the largest single object I have printed so far, shortly after this photo I did start to wonder if it would actually come off of the build platform at the end of the print?
The print is only 17 layers high, 4 White layers all solid, 4 Blue, 6 Red and 3 Green.
Printed at 80mm/sec the total print time was just over 90minutes.
It popped off the bed when cold, not a single bit of warp.
All of my machine now have a T-slot frame around them, this allows me to fix all the electronics, power supply and cables onto and into the frame, it also doubles as an essential filament holder.
The Electronics are housed in the same style enclosure I have used before, with cooling fan.
An ATX Power supply is fitted to the T-slot frame to supply power for the electronics and heated bed.
Last video of the completed build, just some wiring to do and it will be running !
I had many other suggestions on how to make it look 'British' including a great one from Bob "hang a teabag on it!"
Short of printing a bowler hat and walking cane I still think it needs a little more eccentricity and quirkiness, but I'm sure it will evolve over time to have some of those quintessential British qualities.
It's not fully built and completed yet, but I hope to get it fully running for the next local Reprap meet-up.
I started with 75M of 3mm Plastic filament 25M of each Red, White and Blue and only printed one complete set of parts. At the end of this print run I had less than 40cm of each, which was just enough for a Starfish.
Thanks again for reading and I hope you decide to source something from a local supplier today, happy building.