Sunday, 3 December 2017

Christmas Advent 3D Printing 2017 Day #2 - Brassfill & ReForm rPLA

December advent calendar - modular Christmas tree
3D Printing advice #Day 2.

For the background and introduction - Day #1 Post click here

Christmas Advent 2017 Download on Thingiverse here - designed by Tom Van den Bon  With some help for each day by the South African Makers team.

The original advent calendar from 2012 is on Thingiverse - designed by from Peter Leppik.

I'm on Day #2 of the calendar, and today the gift is designed by Tom Van den Bon. It's a mini spool of 3D Printing filament :)

Day #2 of Advent 2017.

The mini-spool is designed to be printed in three parts, the coils are going to be made using Colorfabb Brassfill. Read below, this is a tricky material!

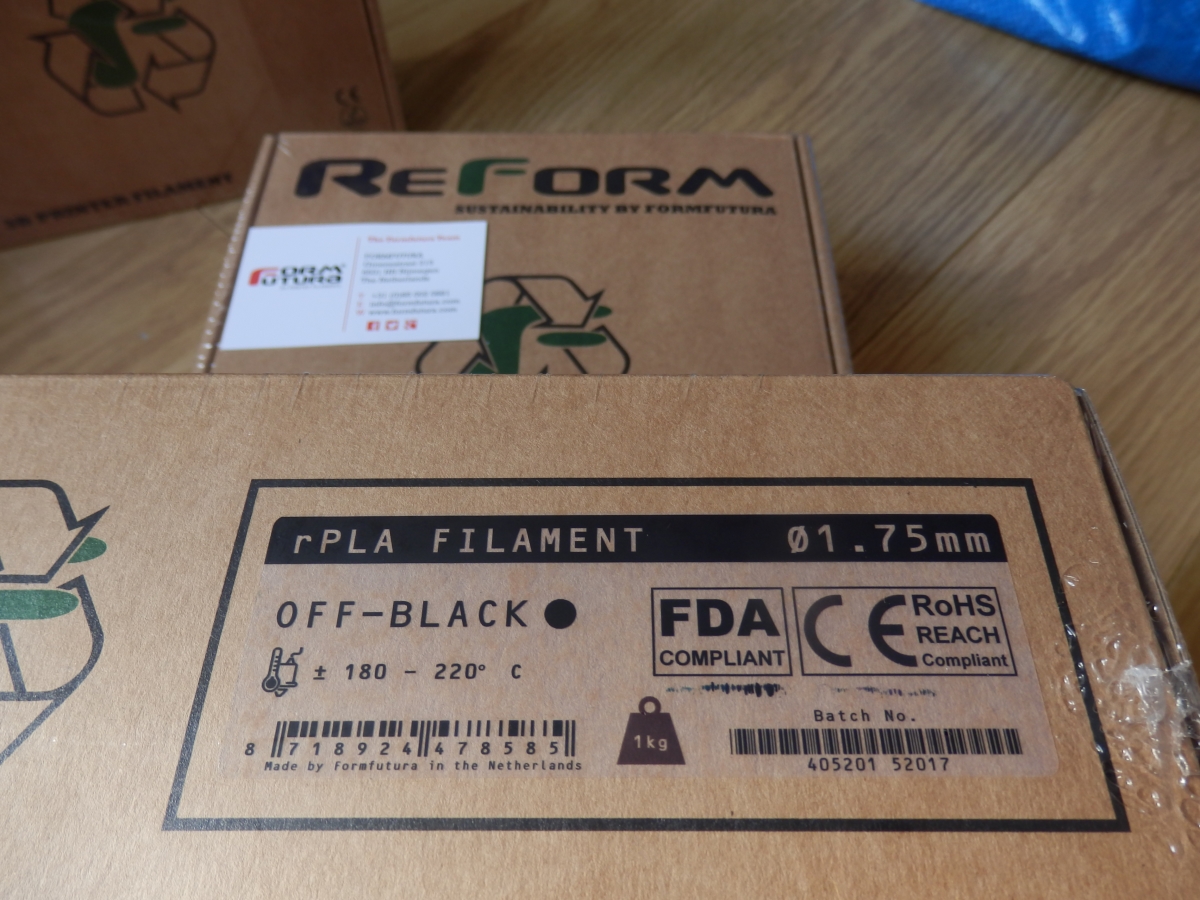
There was only really one choice for the spool, it had to be made from recycled plastic, so I'm using ReForm rPLA filament from Formfutura. This filament also comes as standard on a cardboard spool, and cardboard box. It's really easy to use and provides great results.


Formfutura sell rPLA, rPET and rTitan materials all recycled plastic and on cardboard tubes. I have been using these for months and currently it's my top pick of sustainable #3DPrinting consumables.

Formfutura Recycled rPLA - printed on the LulzBot TAZ6

I'm also testing out other recycled materials (and very interested in any others...), so do check back for more materials and to see what suppliers are promoting both recycled materials and sustainable packaging.

Mini-spool (outer) printed in Formfutura ReForm rPLA.

Mini-spool (Inner coils) printed in ColorFabb Brassfill (1.75mm).

If you manage to get a completed and finished 3D Print - Congratulations! That really is great and 99% of the work. But next you will probably want to polish / shine the Brass object (My Precious!).


You have lots of choice for metal polishing - you can tumble the part, sand it, use some industrial polishing compound, or an off-the-shelf metal polish.

I mostly use a combination of Autosol to start, then some Brasso and some brass/copper polish to finish.

Next you need some polishing devices / brushes, pads, sandpaper or other lightly abrasive things like steel-wire wool or a scouring pad.


I almost always use a shoe cleaning brush (brass/suede type) Shown above from Clarks.


A selection of other brass / nylon (even a toothbrush) brushes are a good idea.

A micro-fibre cloth is really essential too.

You can decide to sand the part first, but I often jump straight into brushing / polishing.


Add some Autosol polish and brush with the Clarks shoe brush - brass side - brush along the layers, not across them.


After a few minutes you should have the following buffed-up with the brush and polish.

Now you need to do more brushing, and ideally use an abrasive pad (dish-washing- scouring pads are ideal).

Remember to also use the micro-fibre cloth and a little Brasso to get the shine back. When things look smooth enough for you (you may not want completely smooth) - I like to still see the 3D printed texture on my parts.

You could carry on, and end up with an even more gold like finish. I stopped here because I wanted some texture to remain.

There we have it. Day #2. Done.


Printing advice - 

I will focus the advice below on Brassfill as it's quite tricky to use...

Before deciding to use Brassfill, be aware it's still listed as an experimental (beta) material by Colorfabb. It's more delicate and tricky to use than both Bronzefill and Copperfill.

But it does look great, feels heavy (quality) and can be polished to a gold-brass finish.

What settings did you use? - 210 Degrees C and a 60 Degrees C heated bed.
0.2mm layer height is fine, but you can go lower. Use a 0.4mm nozzle or larger - don't use really tiny nozzles under 0.4mm, they will clog.
Use a higher number of top/bottom solid layers (I use 5 @ 0.2mm) to give a good finish.
Print speed - it's good from 10mm/sec to around 60mm/sec - Don's be too aggressive on your extruder feed and retraction - I usually turn down retraction speed to 15mm/sec (normal is 32mm/sec).

Also use a lower travel speed, just to stop sudden movements breaking the filament being fed into the extruder. I use 100mm/sec Travel rather than the normal 185mm/sec

Add around 20% to your extrusion multiplier (120% total) for Brassfill.

Don't print more than one object at once - you will have more success with just one object in the middle on the build platform.

16% infill and two perimeters for this model.

Why use it? - It's still the only true Brass filament (I believe?) and it can have amazing & unique results.

Is it strong? - Not really - In filament form (especially 1.75mm) it's really delicate to handle, and gets more brittle over time sat on the reel. You need to be very careful when feeding it into your machine. The filament coils do not want to be forced out of their existing bend radius. It's also not good to use it in a bowden tube configuration.When printed it has very good layer bonding, with a matt slightly rough finish. Polished parts feel strong and high-quality because it's such a heavy material. 

Small printed features will snap off models, small parts are quite brittle even when printed. It's best used for a bust, or solid model with surface features you want to show off / polish, rather than spindly 'tree-like' objects.

Is it easy to use/print - It's straightforward in terms of settings, but handling the material and choice of extruder is quite hit-and-miss for many users. Make sure your extruder is not clamped too tightly onto the filament (it will bend/break/buckle/grind, jam) - Use 200-210 Deg C settings to start with, then tune print speed for ability of the extruder - My advice would be not to print unattended because the filament may/will break and require you to re-insert etc. It snapped three times during this model print. Pause, remove filament end, re-insert coil and continue.

Do you have to dry it before/after use? - No (but keep reading) - Keep it dry and sealed in the bag. My top-tip for Brassfill is if you notice the coils are becoming brittle, dry and also warm up the filament on the reel (in a low temp oven). I have found this tends to make it easier to handle, it becomes less brittle and also prints more smoothly. 

Do i need a 'special' nozzle? - Yes, it's 'soft', but still abrasive. Use a 0.4mm or bigger nozzle. It will work fine with Stainless, Hardened steel, or Ruby nozzles. If you manage to use an entire reel, you may see some slight nozzle enlargement with Brass nozzles.

Does it smell when printing? - No

Does it come on a eco friendly spool? - No, it's the normal ColorFabb (PC) Polycarbonate Spool, but we hope to see Colorfabb introduce Eco-friendly BioFoam PLA spools in 2018. Stay tuned for more info.

Conclusion for ColorFabb Brassfill - Great when you get skilled in using it on your machine, (warning expensive failures!) - It can produce a fantastic, unique and stunning finish. You just need to handle it carefully. Also be aware you do not get quite as much volume on a spool, it's a heavy, quite costly material, but so worth the effort. 

Final note - Always (without fail) clean the nozzle after using this filament! Do not let it sit in the nozzle at print temperature for any length of time when not actively printing. You have been warned, it's not a friendly to use filament it can cause you days of pain and hassle if you are not careful...


Day #2 Completed. That's another object I want to both keep, and have on show this Christmas - and it also has a story to tell about how it became so shiny...

Join me next time for Day #3

Thanks for reading.

Rich.

Please join me on Twitter @RichRap3D

My profile and posts over on Google+

Files and designs shared on YouMagine

Files and designs shared on GitHub

Files and designs shared on Repables 


My Youtube channel is here, all 3D Printing and Hi-Def video content.

Saturday, 2 December 2017

Christmas Advent 3D Printing 2017 Day #1 - Intro, update and print advice.

During December I'm going to be 3D Printing a NEW advent calendar - modular Christmas tree and giving some 3D printing & materials advice along the way. 

Anyone who has been involved in 3D Printing for a while, may remember that in 2012 a wonderful advent calendar popped up on Thingiverse from Peter Leppik. See below, and please read on...

This December printing is not just about a set of 3D models, I'm going to try and make it a useful adventure - you may learn about a different 3D printing material, setting or top-tips.

Along with a lot of people, I also printed out this original modular design in 2012, each December day with my daughters, in a variety of colours and materials. -Also using a few multi-colour-layering techniques on some of the models, you can see below. It was a lot of fun for all of us at home and in the wider 3D printing community.

My full blog post about the original 2012 design by Peter can be found here.

The original 3D Printed Christmas Tree from Peter Leppik (Printed during December 2012).

Almost every year since I have thought about making a new advent calendar, but never found the time to invest in the design and creation.

This year I'm really pleased to say that a new modular advent Christmas tree has been designed by Tom Van den Bon  With some help for each day by the South African Makers team.

The new remixed modular advent design can be found here on Thingiverse, and will have a new model released each day of December.

You can print out all of the tree straight away, but maybe think about how you want it to look when finished. You can see my print above had a lot of different green filaments (my favourite colour).

Image by Tom Van den Bon

The first model for Day 1 is by Shaun Nadan - Fire for the fireplace.


Before we dive in - 

Let's maybe take a little look at the current state of  'fun/consumer' 3D Printing and the future -

Why do this? isn't it just a waste of plastic? - Anyone that follows me will know I not a fan of wasting plastic/packaging, especially with so much ending up having such a negative impact on our environment, for decades to come.

I really don't like printing objects just for the sake of it, it's one of the reasons I have mostly been doing practical 3D printing projects, and using 3D printers as a useful tool for real needs this year.

Many users of 3D printers now churn out a constant stream of whatever the must-print model this month is. I'm trying to limit my random output to testing materials, printing useful objects, models I want to display or use, and the occasional showpiece.

In 2018 I want to be back designing many more my own models/objects and printing them for innovation, development and further adventures in this wonderful 3D printing journey, I hope you carry on following and share the ride with me. I do not intend to waste plastic/materials printing 'stuff'.

So, back to why I'm printing this new Christmas advent calendar. Well, the original set of 52 3D jigsaw prints is used every single year as a focal Christmas decoration, it has started many conversations with people about the good, bad and hype around 3D printing. And it's still loved by our family.

With this new set of advent models, I intend to test out some of the 3D printing filaments I have not had time to look at, and many materials I like using because of their unique properties, look or feel. I hope you find it useful, and do please ask questions - ideally over on Twitter if possible @RichRap3D

I'm also continuing to test out both the original Olsson Ruby nozzle V6 0.4mm and the new Olsson Ruby high flow nozzles (V6 Volcano compatible) in 0.4mm, 0.6mm and 0.8mm versions.


This is a really good test set of objects for the Ruby nozzles as it's going to cover many different machines, materials and settings over the next ~25 days.

Day #1 - 

First up, the lower sections of the tree (trunk) - It's got to be a wood filament really, and one I have not used for a while is Fillamentum Timberfill (Cinnamon)


Printed on the Prusa i3 MK2 (original) with a V6 0.4mm Olsson Ruby Nozzle.


What settings did you use? - Go slightly lower temperature than a normal PLA, I use 180 Degrees C for Timberfill (may need to go even lower with some other wood filled materials).
I often use 0.2mm layer height (It helps the wood-grain look) and a 0.4mm nozzle or larger - don't use really tiny nozzles under 0.4mm, they will clog.
Use a higher number of top/bottom solid layers (I use 5 @ 0.2mm) to give a good finish.
Print speed - it's good as 30-90mm/sec - Not so good at really low speeds (under 15mm/sec) because it likes to expand and ooze out of the nozzle - many wood and 'filled' materials can do that at lower speeds. You can combat some ooze by lowering temperature, but watch out for lower layer bond strength or weak extruders jamming (use a good extruder, geared preferably).
16% infill and two perimeters for this model.

Why use it? - It's an easy to print wood filled filament, looks good and can be sanded, drilled, tapped, even stained after printing. I think it also looks the most 'woody'.

Is it strong? - When printed it has good layer bonding strength, it's slightly weaker to handle than normal PLA and be careful with the filament - especially in 1.75mm it can snap if not handled carefully and spooled nicely into the machine.

Is it easy to use/print - Yes, you can use a lower temperature PLA settings to start with, then tune retraction distance and print speed v temperature depending on what sort of model you are printing - big/small.

Do you have to dry it before/after use? - Yes/No - Keep it dry and sealed in the bag, it will take on moisture and that will affect print quality, fine angel-hair like stringing, gaps and generally more ooze if it's not dry.

Do i need a 'special' nozzle? - No, it's not abrasive, just remember to use a 0.4mm or bigger nozzle. It will work fine with Stainless, Hardened steel, Copper, Ruby or Brass nozzles. Many filled filaments can tend to collect debris and runny material around the nozzle, so clean before and after use.

Does it smell when printing? - Yes, like MFD (wood fibre board - when you cut it) I unfortunately don't like the smell at all.

Does it come on a eco friendly spool? - No, but it is marked ABS with a Recycle symbol - foil bag and cardboard box.

Conclusion for Fillamentum Timberfill - Good, wood like finish, no problems or failures. I always clean the nozzle after using filled filaments (especially wood), inside and out with a section of Nylon at a higher temperature. It will have some resin-like sticky residue after printing, so get it cleaned ASAP.

Day 1 present - This is a nice flame model for the fire, it's just asking to be printed in at least two orange/red?/yellow colours.

There are so many nice orange shades, but since I used Fillamentum Timberfill for the base, I have selected two more Fillamentum PLA's to compliment the Day 1 gift -


PLA Extrafill "Melon Yellow" and PLA Extrafill "Luminous Orange"

For this we will pause the print after the fire background is printed in Luminous Orange and insert the Melon Yellow, then continue the print. Most 3D printers should allow you to pause a print and change colour. If yours does not you may be able to cut the filament and manually feed in the next colour during the print, it's a little risky and some extruders may not like you doing this, but it can work well.


The Prusa i3 also has the option of using 'Colorprint' to set points in any model to automatically pause and allow a material or colour switch.

Settings for most PLA's are really quite standard now, 190 Degrees C with a 60 Degrees C heated bed. 0.2mm layers and 0.4mm nozzle with 0.9mm extruder retraction on the Prusa i3 MK2.


Day #1 Completed. I think it turned out nice, feels warm and inviting. This is going to be a big tree...

Join me next time for Day #2

Thanks for reading.

Rich.

Please join me on Twitter @RichRap3D

My profile and posts over on Google+

Files and designs shared on YouMagine

Files and designs shared on GitHub

Files and designs shared on Repables 

My Youtube channel is here, all 3D Printing and Hi-Def video content.


Friday, 9 June 2017

3D Printing Adventures Summer 2017 update

Summer is coming up fast, so here is an update on my current and future 3D Printing adventures.

Firstly the 3D Printing for Dummies book has now been issued as a revised and updated Second Edition, I was surprised to receive the author copies as I was not expecting it to be published until mid-late summer.


But here it is, and thank you to everyone who contributed to it's updates and revisions. Also a big thank you to my co-author Kirk and the great team at Wiley for making this update happen.


Some really great projects, printers and material updates have been added to the book, along with a lot of updated topic's and sectors where 3D printing is growing.


I can only find a USA link for the new version, but worldwide stocks should be available soon if you wish to buy a copy. And if you do, thank you.


I go over a lot of updates in the video below, and here is also a quick-jump index if there is something specific you want to hear about -

Quick jump index -
00:50 - 3D Printing for Dummies (2nd Edition)
02:10 - The Olsson RUBY Nozzle
02:26 - The Sorceress - printed with the Ruby
02:40 - Pongo PLA - interesting translucent white
03:20 - PEI Print bet 3M sheet from AndOrNot
03:50 - Fuel3D Scanner is no longer for sale :(
05:15 - Polymaker Polysher & Polysmooth Kickstarter
06:08 - Glitter machine...
08:27 - Sigma R17 Noodle catcher upgrade
09:25 - Learning SharkCAD3D V10
10:00 - 100% Recycled Filament by ReFlow

You can also find this and more on my YouTube channel in HD over here


Olsson Ruby nozzle - 

I was very excited to receive an Olsson Ruby nozzle for testing, this is an upgrade I have been fascinated about for some time. I'll be doing a lot more testing, but the initial results are very smooth and it's printing really well on the Prusa i3 MK2.


The construction is quite simple, but exceptionally engineered. This has a real ruby embedded inside the tip of the hot-end with a 0.4mm nozzle hole.


The back is plugged and then drilled out to allow a 1.75mm or 2.85mm filament path.


They are E3D and Ultimaker Olsson block compatible.


It's easy to fit - as always, be careful with fitting, and I would certainly advise to lock the heater block and thermal break down on to the nozzle, rather than trying to screw the nozzle tight into the heater block directly. 
When fitting any E3D nozzle I always leave a small gap with the nozzle because for the E3D V6 the stainless steel thermal break is designed to lock flat to the nozzle, not for the nozzle to seal against the heater block.


This image does not do justice to the great model by Louise Driggers (The Sorceress) you can get it from Pinshape here  but I wanted to show a print from the Olsson nozzle - this is printed at 0.2mm layers in Fillamentum  PLA Rapunzel Silver

The finished print quality looks like you would expect from a 0.15mm layer height. But I will do a lot more testing with the Ruby nozzle - especially with filled and composite filaments.


Many thanks to Pongo for the 'water clear PLA' filament sample. We had a discussion over on Twitter about this material - I'm looking for translucent white (not clear, but also not opaque) filaments to use as Optical LED light guides. This looks very promising, I'll update you on the results.


Andrew from AndOrNot sent me over a new sample (Test) bed material (3M sticky-backed PEI Sheer) - It's going to be fitted to the Sigma R17 glass bed so I can print PETG without damaging the glass build surface.


Polymaker Polysher (Kickstarter)

I'll have a dedicated post all about the Polysher and Polysmooth materials, I have done a lot with the machine and am impressed with the results, here is a quick overview example below -


The Polysher and Polysmooth materials are now becoming available around the world. For an overview and feedback from early users, do take a look at the Kickstarter here.


Don't print at these high (210 - 230) temperatures! - Really it's way too high - I'm printing around 190 for 55mm/sec print speeds and that produces great results without micro-bubbles or angel-hair.


I'll talk more about temperature and print settings for Polysmooth in the next blog post and video, but do take a look at the simple temperature test above - and as it's a constant speed spirial vase, no retractions or pauses were experienced, so it's a good test for material temperature stability.

Before (Top) and After smoothing (Bottom) - This was a 'draft mode ' print made quickly at 0.2mm layers - it's quite small and detailed, but the Polysmooth helped make it a really great finish.

Voronoi D Tower 
Math Art by Dizingof


Testing out the transparent Polysmooth - Above shows both Clear and white - they both become flat smooth, but the internal layer lines remain for the clear material, the surface feels smooth for both.


Another example above - white, natural and clear, smoothed in IPA for around 35 minutes. Make sure you watch out for fluff and dust because it'll stick and bond into the surface finish (see lower left above).

Designed by  Mark Durbin (MakeALot)

For Sigma R17 and TAZ6 updates, do check out the video above. I'll have a lot more on these machines, projects and developments over the summer.

SharkCAD3D V10 - 

I have also been learning a new 3D CAD package (SharkCAD 3D V10) From Punchcad )


So far I'm really impressed with this package, It's amazingly powerful and has a lot of great 3D printing features for both design and model processing. I'll be posting a lot more about this package as I learn how to use it over the following months (and years) - This is going to be my new CAD software for all existing and future developments from this point on.

If anyone is interested in me posting some training video's or anything specific about this software, and it's capabilities, do let me know. It'll help me learn, and after doing a lot of screen-casting last summer I would like to do more.

Punchcad also have ViaCAD 2D/3D and many other SharkCAD packages at very low to high price points, so something for every maker or 3D design professional. I would encourage you to check them out, if for no other reason than the fact I accidentally stumbled over them, and was amazed I didn't already know they existed.

It's still early days for me learning the tools and user interface, but I'm quite sure you will be pleasantly surprised if you decide to try out the trial software or buy a version (Mac and PC available).


Quad Extruder printing? - 

I also hope to receive my Quad extruder upgrade for the Prusa i3 MK2 at some point in the next month. The Prusa team have quite a big backlog of orders and I didn't place my order until October, so the September shipments are going out first. I'll keep you updated on the progress with that, but I'm excited to get hold of it and experiment with multi-materials and colours.

ReForm Recycled filaments - 

And just as I was editing this video and blog post, I received some really nice 100% fully recycled 3D Printing filaments - You can find out more here - > ReForm by Formfutura


Cardboard spools, 100% recycled rPET, rPLA and rTitan materials. It's exactly what I have been asking suppliers to make for many years now.


I'm really impressed that Formfutura have managed to manufacture these materials, I hope they print well and I also hope more manufacturers will also think about sustainable materials and packaging for 3D printing filament consumables.


I'll let you know very soon how I get on with these materials, spools and how they perform in various 3D printers.

I hope that was a useful update, lots more to come from me this summer -  do comment and please subscribe to my YouTube channel for more 3D printing adventures soon.

Thanks for reading and watching.

Rich.

Please join me on Twitter @RichRap3D   -  https://twitter.com/RichRap3D

Files and designs shared on YouMagine - https://www.youmagine.com/users/richrap

Files and designs shared on GitHub – https://github.com/RichRap

Files and designs shared on Repables - http://repables.com/u/richrap/

My Youtube channel is here, all 3D Printing and Hi-Def video content.


Sunday, 30 April 2017

TAZ6 Octo-Tool holder and a reminder that thermoplastic can be reformed after 3D Printing

TAZ 6 Octo-Tool holder. Design, 3D print and post thermoforming


Last month we saw a lot of people 3D printing the hairy lion. That inspired me to design a complex looking tool holder, but with an easy way to 3D print out the model and some easy re-shaping of the tentacles after printing (using hot air for thermoforming).

Inspiration for this idea came from the Hairy Lion model by Primoz Cepin

The hairy lion is a good example of re-forming thermoplastic into a different shape after first printing in a much easier model, that's more optimised for the 3D printing process.

I made a video about the design, and how to shape 3D printed parts after 3D printing below -


You can also find this and more on my YouTube channel in HD over here

The model is printed out flat. It's easy to both model and 3D print this way.


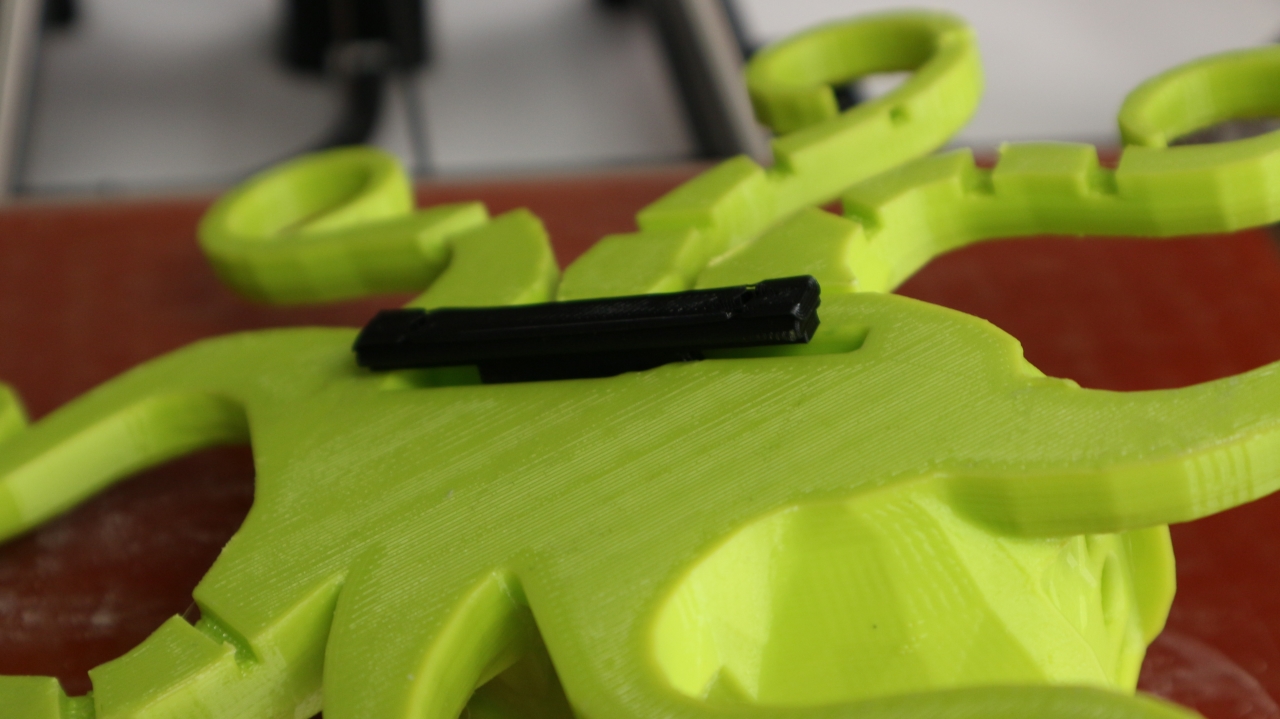
After printing, shape the legs into interesting positions by using a heat-gun. This is Colorfabb nGen material, great for thermoforming. PLA is also very easy to form using hot-air or hot water.

The metal plate shown above is simply being used as a heat shield so the tentacles bend exactly where I want them and the body is not deformed.


You may need to do a little more bending once fitted to make sure tentacles are not in the way of the 3D printer moving parts.


A 3D printed clip allows you to slide the Octo-Tool holder onto the machine.


You just need to slot the clip into the TAZ 6 20mm aluminium t-slot section on the left hand side.
You could add many other tools and upgrades to your machine this way.


You will need to remove one part of the TAZ 6, just to allow the clip to slot in. Be careful not to loose the t-slot nuts, they do enjoy slipping down the aluminium channel sections. Use blue-tack to hold them in place.


The top tool holder can also be printed and fitted, if you would like to have a different top tool holder, then feel free to alter the Freecad model included with the Youmagine link below.


It can be fitted using the existing bolts, just loosen then a little and slot in the top tool holder.


Add tools and SD cards, and you are all set with even more awesome TAZ 6 3D Printer.

I have posted the design files for these models and the STL's for 3D printing along with advice for assembly onto your TAZ6 are over on Youmagine here

The original original Bucket O' Octopodes (thicker legs) - by moleofproduction can be found here - http://www.thingiverse.com/thing:8896

2D Scanning for accurate 3D models
One tip I didn't talk about in the video above is an easy way to make shapes for tools like the Pliers.

I have used this method many times and it's a great way to ensure existing objects fir into 3D printed parts.


Take a 2D scan or a good photo, or the object. Then just load (import) this image into your CAD program and scale to a known dimension of the object. For this set of pliers, I measured the distance of the middle round section and scaled the image so that dimension was correct. then you know you are at the correct scale for the model.

It's then just a case of tracing around the image and producing a plane you can extrude, to form an indent for the object. You can round corners and add grip points as I did in the top tool holder.

I have replaced all manner of objects using this method, from shower mounts to kitchen utensils, just from simple 2D scans using a flat-bed scanner.

I hope that was useful, do comment and please subscribe to my YouTube channel for more 3D printing adventures soon.

Rich.

Please join me on Twitter @RichRap3D   -  https://twitter.com/RichRap3D

Files and designs shared on YouMagine - https://www.youmagine.com/users/richrap

Files and designs shared on GitHub – https://github.com/RichRap

Files and designs shared on Repables - http://repables.com/u/richrap/

My Youtube channel is here, all 3D Printing and Hi-Def video content.